January 31, 2026
The Transition from Mechanical Stress to Electrical Microstructure
Last week, we discussed the applications of V-cut and Mouse Bite in panelization to solve mechanical stress issues. This week, we shift our focus to the more microscopic electrical dimension—Back Drilling.
As the high-speed era of 25Gbps, 56Gbps PAM4, and even 112Gbps arrives, the often-invisible Via Stubs on PCBs have become the number one killer of Signal Integrity (SI). This article will deeply analyze the physical mechanism of back drilling technology, factory processes, layout specifications, and demonstrate how eCloud PCB achieves the ultimate process of controlling stub lengths within 5 mils.
In multilayer board design, when a signal transitions from the Top layer to an inner layer (e.g., Layer 3) for transmission, a standard Plated Through-Hole (PTH) passes through the entire board thickness. The section of the "metal tube" from L3 to the Bottom layer that is "not connected to any trace and left floating" is the Via Stub.
In low-speed circuits, stubs have minimal impact; but in high-speed circuits, a stub acts like a parasitic capacitor and an open transmission line.
Parasitic Capacitance Effect: According to the rule of thumb, the parasitic capacitance density of a via stub in FR-4 material is approximately 0.2 pF/100 mil. A 100-mil stub introduces about 0.2 pF of capacitance, causing a sudden drop in impedance on the high-speed signal path, leading to reflections and signal jitter.
Quarter-Wave Resonance: This is the most critical effect. When the stub length equals 1/4 of the signal wavelength, the reflected wave cancels out the incident wave due to phase opposition, causing the signal energy at that frequency to be "absorbed," creating a deep dip in the Insertion Loss (S21) curve.
Resonant Frequency Formula:
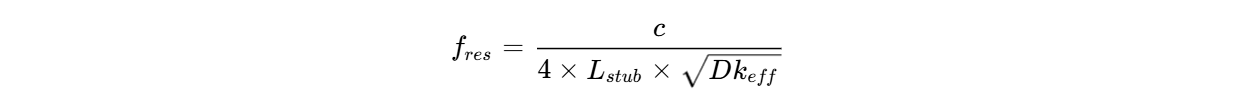
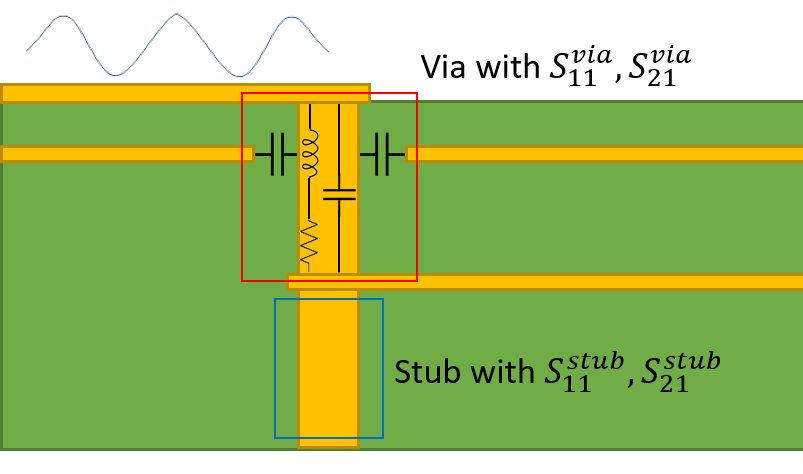
Via stub within a circuit model. There is parasitic capacitance with and around the via and its stub. These parasitics modify the via’s impedance as some function of frequency.
| Stub Length | Resonant Frequency (approx.) | Applicable Maximum Rate | Key Conclusion | | :--- | :--- | :--- | :--- | | 100 mil | 15 GHz | < 5 Gbps | Not suitable for high speed | | 20 mil | 75 GHz | ~ 25 Gbps | Standard back drilling specification | | 10 mil | 150 GHz | ~ 56 Gbps | Gold standard for 25Gbps+ | | 5 mil | > 250 GHz | 112 Gbps+ | eCloud PCB's Precision Process |
"Back drilling" uses a slightly larger drill bit than the original via, entering from the backside to precisely cut off the excess copper wall of the stub. This is a process with extremely high requirements for depth control.
How to ensure the drill bit cuts the stub without damaging the effective circuit layer just a few mils above?
The back drill hole diameter ((D_{backdrill})) must be larger than the original via diameter ((D_{via})) to allow for alignment tolerance.
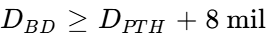 .
During the layout phase, engineers must precisely define back drill rules to avoid production disasters.
In EDA software (Altium/Allegro), it is necessary to define which vias require back drilling (e.g., drilling from Bottom to Layer 3).
Back Drill Size Calculation:
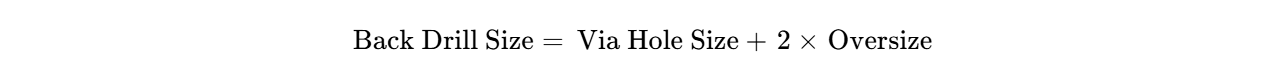
This is the most error-prone step. The back drill hole is larger than the original hole, so surrounding traces must be avoided, otherwise they will be drilled through.
Keep-out Diameter Calculation:
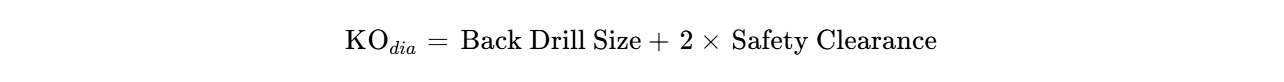 Example:
If Via=10mil, Back Drill Oversize=5mil, Safety Clearance=8mil.
Then Keep-out Diameter =
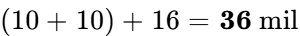
Back drilling removes metal, increasing the impedance in the via area. To maintain Zo (Characteristic Impedance) continuity, anti-pad sizes need optimization, and even shrinking the anti-pad on back-drilled layers appropriately to compensate for capacitance loss is recommended. 3D simulation (e.g., HFSS) verification is advised for 25Gbps+ signals.
In designs for PCIe Gen5 (32GT/s) and 112G PAM4, the traditional IPC Class 2 standard (Stub ~ 10-15 mil) is stretched thin. eCloud PCB, focusing on high-end prototyping and small-batch production, offers solutions that exceed industry standards.
For 112Gbps PAM4, the signal bandwidth extends to 56GHz.
A server client faced BER (Bit Error Rate) exceeding specifications during PCIe Gen5 testing. Analysis revealed the original manufacturer's back drill stubs averaged 13 mil. After switching to eCloud PCB's 5mil process, Return Loss improved by 3dB, eye diagram opening increased by 15%, and certification was successfully passed.
From last week's V-cut to this week's Back Drill, we have witnessed the evolution of PCBs from mechanical support structures to electrical performance enablers.
For high-speed designers, "Zero Stub" is the ultimate goal. Although Blind/Buried Via technology can also solve the problem, considering the trade-offs between cost and process complexity, back drilling will remain the mainstream choice for high-end boards for the next 5-10 years.
Key Takeaways:
We hope this report serves as a practical guide on your desk. If you have more questions about high-speed manufacturing processes, feel free to discuss!
