High Aspect Ratio PCB Design and Manufacturing Challenges
 As products evolve towards high computing power and high density (especially AI servers and high‑end GPU carrier boards), PCB layer counts have surged from the conventional 8 layers to over 30 layers. To cram more interconnect signals into a limited board area, the via hole diameter must continuously shrink. This double squeeze of “increasing board thickness and shrinking hole diameter” directly causes the aspect ratio to climb sharply. This DFM note will take you deep into the physical and chemical challenges behind high aspect ratios, and how Layout engineers should accurately grasp the design scale.
I. The “Micro‑Tunnel” Challenge of High Aspect Ratios: Why is A/R > 10:1 So Difficult?
An aspect ratio is not just a geometric number; it is a direct reflection of physical and chemical process limits. A hole with a high aspect ratio means the hole body is extremely deep and the hole diameter is extremely narrow. Any material exchange required inside the hole (such as chemical fluid flow, cleaning, electroplating) becomes exceptionally difficult.
1. Mechanical Drilling: The Limits of Drill Bit Rigidity and Chip Removal
- Risk of Broken Drill Bits and Deviation: As the aspect ratio increases, the length‑to‑diameter ratio of the drill bit also increases. Long and thin drill bits drilling into thick boards at tens of thousands of RPMs are highly prone to “deviation” or even breaking. Once a drill bit breaks, not only is that hole scrapped, but the entire board might also be ruined.
- High Temperature and Smear: During deep hole drilling, the narrow space makes it extremely difficult for drilling chips to be exhausted. The high temperature generated by friction will cause the epoxy resin on the hole wall to soften or even carbonise, forming a thick layer of smear that seriously affects subsequent hole wall metallisation.
2. Hole Metallisation: The Test of Throwing Power
Plating copper onto the insulating hole wall is the soul step in establishing interlayer electrical connections. The biggest nightmare of a high aspect ratio lies in the “uneven current distribution” during electroplating.
- The “Dog‑Bone” Effect: In the electroplating tank, the resistance at the hole opening is low and the current density is high, so copper ions deposit extremely fast; whereas in the centre of the hole, the resistance is high, the current density is low, and fluid exchange is difficult. This leads to an extremely thick copper layer at the hole opening and an extremely thin copper layer in the centre, looking like a dog bone in a cross‑section.
- Voids and Open Circuits: In the most extreme cases, copper might not be plated in the centre of the hole at all, forming a void and an open circuit. In addition, if tiny bubbles generated during the electroplating process are trapped in the narrow deep hole and cannot escape, it will also cause copper to fail to plate in those areas.
II. The Golden Rules of Routing and Design: Balancing Performance and DFM
For Layout engineers, the aspect ratio is the bridge connecting design ideals and manufacturing realities. During the layout stage, please be sure to incorporate the following DFM considerations into your specifications:
1. Accurately Grasping the Balance Between Hole Diameter and Board Thickness
- Reduce Unnecessary Aspect Ratios: Under the premise of meeting electrical performance and mechanical constraints, try to choose a thinner board thickness or “moderately enlarge the hole diameter” in areas where space allows. If the signal load is not heavy, fine‑tuning a 0.2 mm hole diameter to 0.25 mm can significantly reduce the aspect ratio and greatly improve the production yield of the board factory.
- Ensure Safe Margins for the Annular Ring: High aspect ratio drilling is prone to slight deviations. When designing, it is recommended that the pad diameter be at least 0.15 mm larger than the drill hole diameter to ensure a sufficient annular ring, preventing the “breakout” phenomenon caused by drilling deviation and ensuring long‑term electrical reliability.
2. Crossing the Limits: Shifting to HDI and Micro‑Blind Via Technologies
When the design density is extremely high and the aspect ratio of mechanical drilling approaches or exceeds the factory’s limits (usually greater than 12:1), rather than rigidly sticking to traditional through‑holes, it is better to decisively switch to the HDI (High Density Interconnect) process.
- HDI utilises laser blind vias with a depth typically spanning only 1 to 2 dielectric layers. For example, with a depth of 60 µm and a hole diameter of 100 µm, the aspect ratio is only 0.6:1. This perfectly avoids the various pain points of deep hole electroplating and is the inevitable development direction for modern high‑density designs.
3. Advance Engineering Confirmation with the Board Factory
There is a massive gap in equipment and chemical fluid capabilities among different board factories.
- The aspect ratio limit for conventional board factories is around 8:1.
- Board factories with a certain level of capability can stably mass‑produce 10:1 to 12:1.
- Only top‑tier board factories (such as those supplying high‑end server boards) can challenge 14:1 or even 15:1.
Before finalising the stack‑up design, be sure to confirm the upper limit of the “stable mass production” aspect ratio capability with your PCB supplier.
III. Cutting‑Edge Solutions on the Manufacturing Side: How Do High‑End Board Factories Overcome High Aspect Ratios?
To meet the aspect ratio demands of 14:1 and above brought by products like AI servers, high‑end board factories must make huge investments in equipment and chemicals:
- Plasma Desmear: Traditional potassium permanganate chemicals struggle to penetrate extremely fine deep holes. High‑end processes employ vacuum plasma, utilising active free radicals to indiscriminately bombard organic matter inside the hole, achieving a thorough cleaning effect.
- Pulse Reverse Plating (PRP): Replacing traditional direct current electroplating. By periodically alternating the current direction (forward plating copper, instantaneously reversing to dissolve the overly thick copper layer at the hole opening), it forces the copper thickness inside the hole and at the opening to tend towards uniformity. This is the core technology for conquering high aspect ratios.
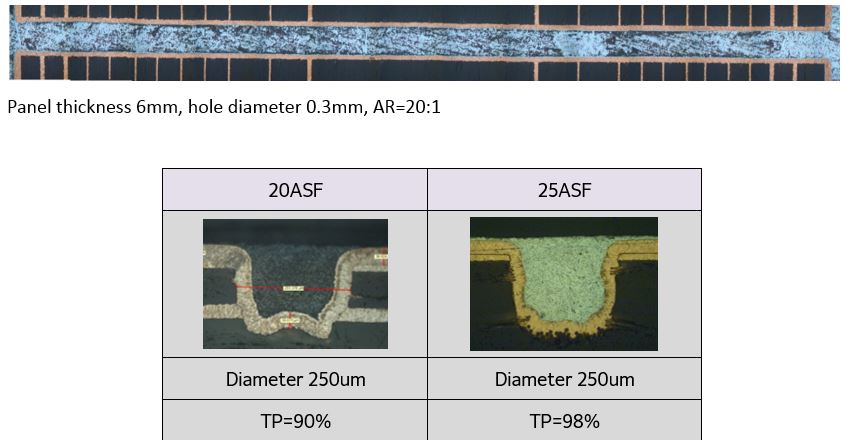
- Vertical Continuous Plating (VCP) and Powerful Agitation: Paired with special electroplating additives with high throwing power, and utilising ultrasonic waves or powerful jet flows, this forcibly breaks the concentration boundary layer inside the hole, “pumping” copper ions into the centre of the deep hole.
IV. Summary
Aspect ratio is not just the mathematical division of board thickness and hole diameter; it is the touchstone for testing the manufacturing difficulty of a high‑layer‑count board. Excellent hardware design must know how to strike the best balance between “extreme routing density” and “factory process limits.” Proactively controlling the aspect ratio in the early stages of design, or introducing HDI laser via designs when necessary, will not only enable smooth mass production of the product but also significantly reduce potential reliability risks, allowing your high‑end design to truly come to fruition.
